Search
Search
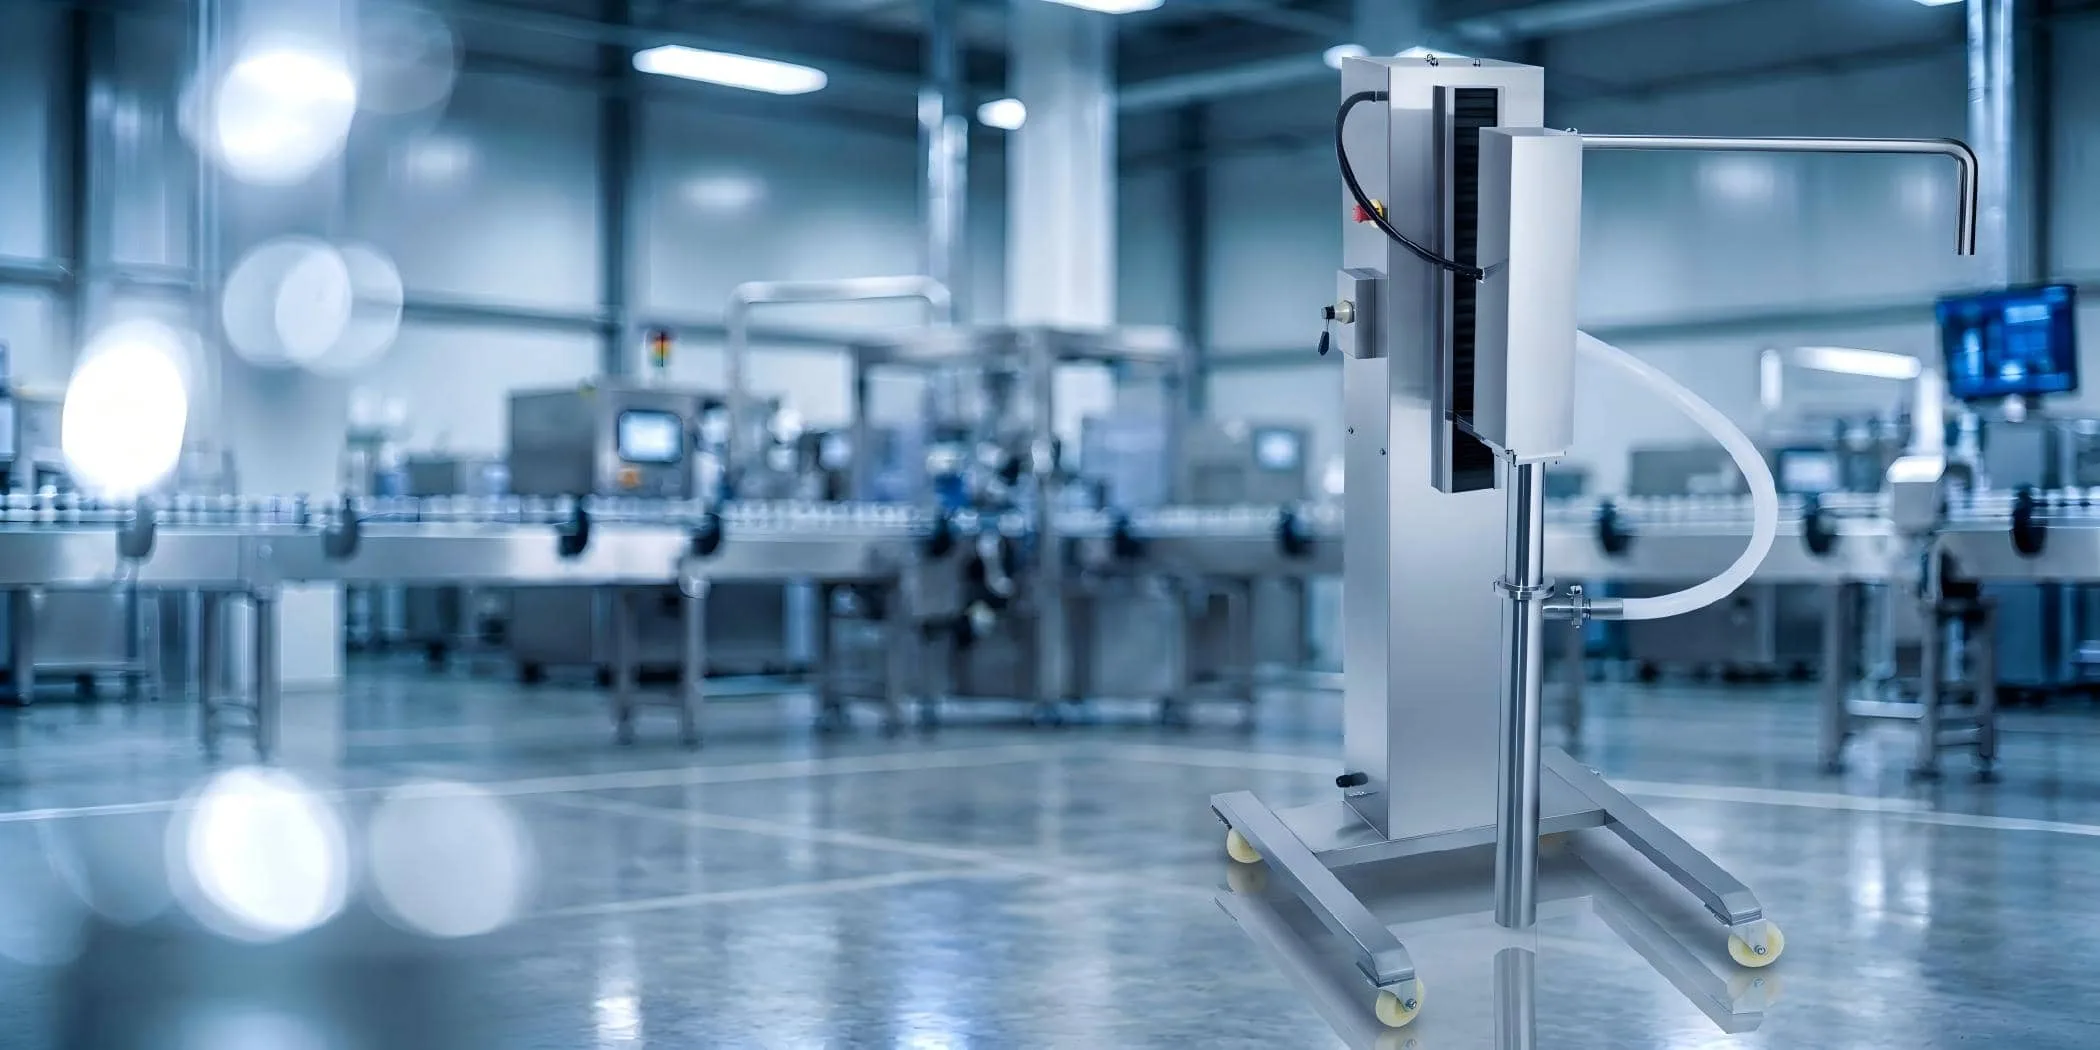
Designed for hygienic, gentle handling of delicate bakery ingredients, our food-grade transfer pumps provide continuous, low-shear pumping of aerated cake batters and semi-fluid doughs without compromising their structure. Built from premium 304 food-safe stainless steel and 6061 aluminum, HSENDA pumps integrate smoothly into automated production lines.
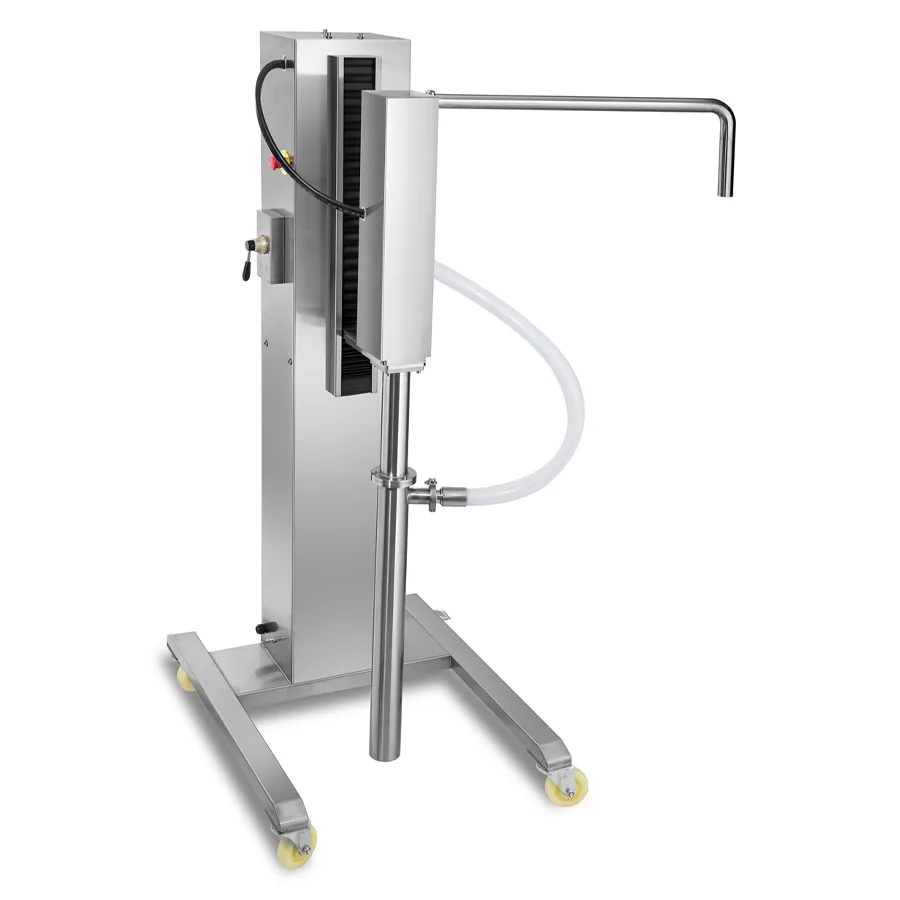
Industrial Food-Grade Transfer Pump TP100
Our advanced pumping systems handle ingredients with a range of viscosities, moving them smoothly from mixers to depositors while preserving their texture and aeration.

Gentle, Low-Shear Pumping
Protect the quality of every batch. Our food transfer pump design minimizes friction, helping aerated batters and semi-fluid doughs retain their density, texture, and structural integrity throughout transfer.

Safer & Smarter Automation
Move beyond outdated and hazardous lifting methods. HSENDA pumps offer a safer alternative to traditional cylinder lifters, transferring batches from mixing bowls up to 650mm in diameter directly to your depositors.

Maximum Food Safety
Maintain high hygiene standards throughout production. Built with durable 304 stainless steel and 6061 aluminum, our food transfer pumps are designed to support safe, sanitary operation and meet international food-grade requirements.
High-Efficiency Liquid & Batter Transfer Solutions
Moving thick batters and delicate creams from mixers to depositors requires reliable equipment, especially in large-scale bakery production. HSENDA provides food-grade liquid transfer pumps designed for the demanding needs of commercial food factories.
Our transfer pump systems help preserve the structure of aerated ingredients while supporting efficient, continuous material handling. Whether you need to move heavy doughs or maintain a steady supply of liquid ingredients, our solutions help automate transfer, reduce manual lifting, and maintain strict hygiene standards.
Not sure which transfer pump is best suited to your batter viscosity?
CONSULT OUR PUMP EXPERTS TODAY